BANANAS / PACKAGING APPLICATION
Forming deep cartons for banana packing
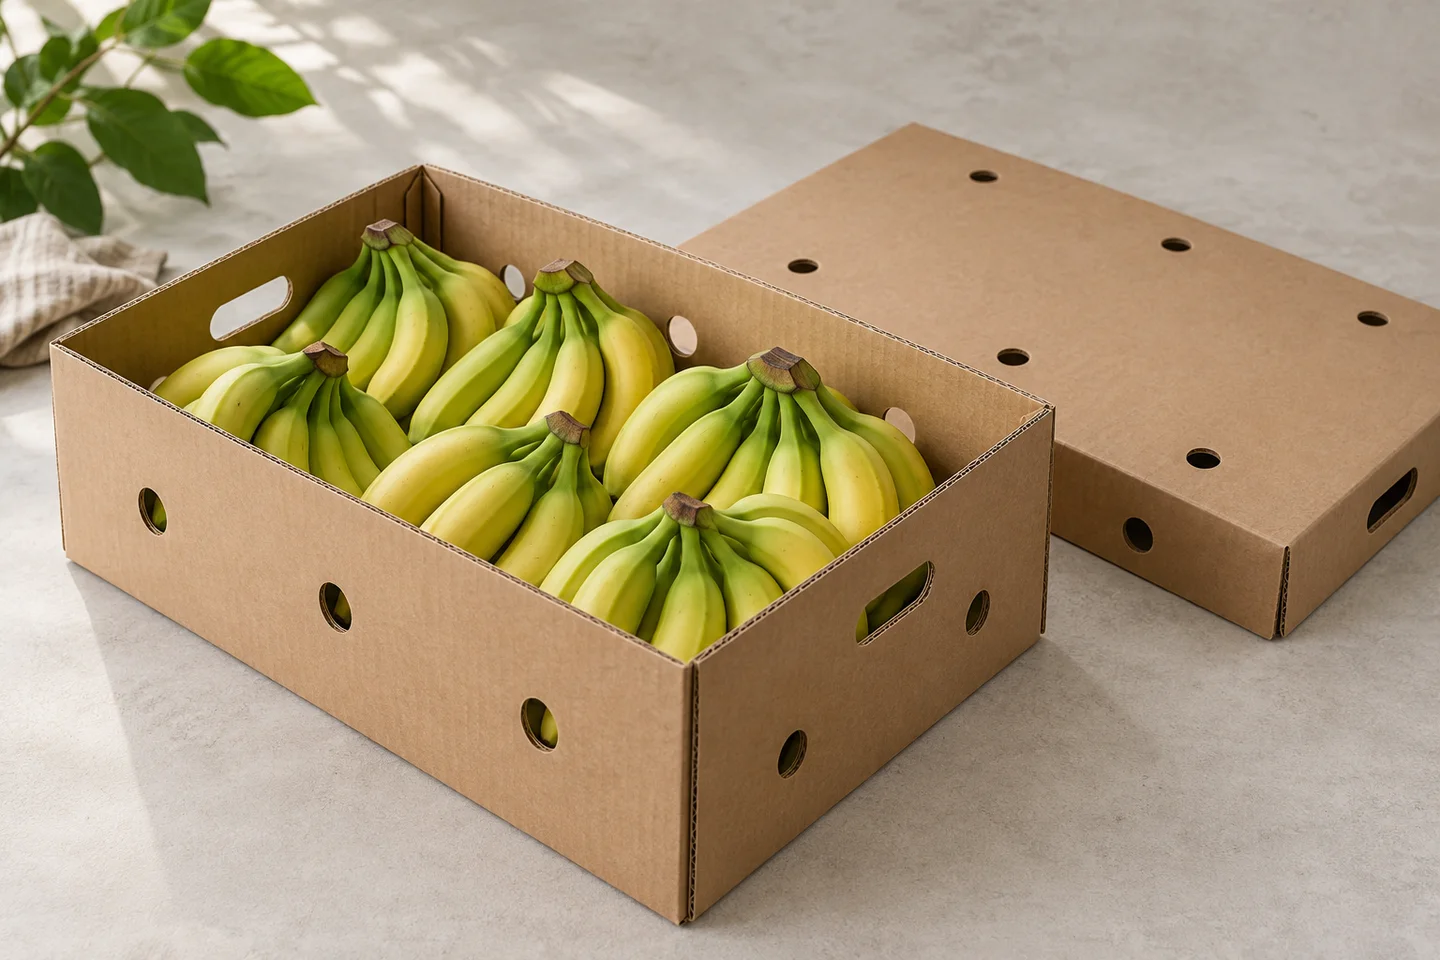
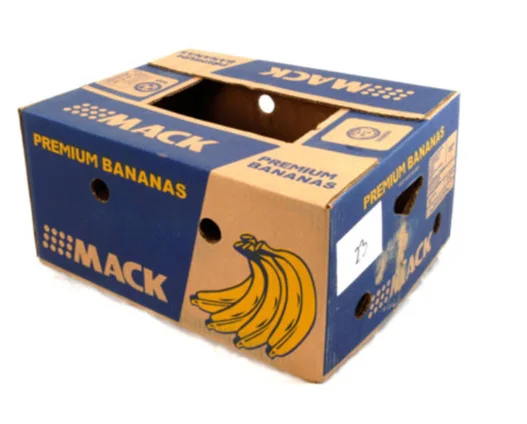
Banana carton forming starts with the depth and construction of the box. The application configuration combines automatic blank feeding, hot-melt glue application and continuous forming for deep corrugated cartons. The supplied banana sample shows a printed box with ventilation openings and hand holes. Xunding reviews the blank, board and packing sequence together, so the proposal describes the box you need to make and the point at which it enters your banana packing operation.
THE REAL CORRUGATED STRUCTURE
Actual box samples
Why the deep banana carton determines the setup
The banana sample is a deep carton rather than a shallow produce tray. Its taller walls, openings and folded joins define how the blank needs to be supported as it is formed. Start by measuring the finished box and showing how the base is constructed. Include photos of the inside corners and any separate cover. The available machine space should be compared with the flat blank as well as the assembled carton, because the board travels through the equipment before it reaches its finished shape.
Printed panels and handling openings should be located on the drawing. An opening near a fold or a joining area can influence where the board is held and where adhesive is applied. If different banana cartons share a similar print, check their dimensions and crease positions separately. A practical equipment review needs the exact production blank. Artwork is useful for checking orientation, but the cutting and creasing pattern provides the information that establishes the feeding, folding and discharge arrangement.
Continuous forming from a stack of blanks
The proposed arrangement uses bottom vacuum feeding to take a blank from the stack. The application description allows the blank supply to be replenished during operation and uses a continuous sequence through multiple forming positions. Automatic hot-melt application prepares the joining surfaces before the walls and folded sections take shape. Servo control, a PLC and photoelectric tracking coordinate the movement. The chain-indexed transport described for this configuration provides the transfer sequence between the processing positions and the point where formed cartons are collected.
For a banana box trial, watch the blank throughout that sequence. Check that one blank separates cleanly, that its printed side remains correctly oriented and that the folds follow the creases without distorting the openings. Inspect the glued overlap after discharge and confirm that the box stands square. These are useful acceptance observations because they relate directly to the empty carton the packing team receives. The trial should use your intended cardboard and adhesive, with the agreed output measured on that same box design.
The reference size and material envelope
This deep-box application specifies a finished length of 200–550 mm, width of 200–400 mm and height of 150–350 mm. Cardboard thickness is listed at 1.5–3 mm, and the configuration output is 20–30 boxes per minute. These ranges belong to this reference arrangement. They should be considered together: a box close to one dimensional limit may still need a different blank layout or folding arrangement. Provide the full drawing and board sample before choosing equipment on a dimension alone.
Board condition is part of the feeding and forming discussion. Record the thickness, grade, printed or coated surfaces, and the crease specification that your carton supplier will deliver. If you buy blanks from more than one supplier, include samples from each source you intend to use. The aim is to agree a configuration and trial material that reflect normal production. The table gives a clear starting point while the final order defines the confirmed box range, tooling and working output for your actual cartons.
Joining, openings and the finished box check
Hot-melt joining should be reviewed against the banana carton’s overlap areas, not added as a generic setting. Identify which surfaces meet, the glue pattern required and any openings that must stay unobstructed. Taller box walls also make it useful to inspect the inside of the finished carton. Look for correctly folded edges and a consistent relationship between the walls and base. If the box uses a separate lid, form and inspect that component as a separate part of the packaging plan.
Agree the empty-box acceptance checks with Xunding and your carton supplier before the trial. Dimensions, squareness, visible joints and opening positions provide an initial checklist. Requirements for a filled carton, pallet stacking or your distribution route belong in a separate packaging assessment using the completed pack. Carton forming cannot establish those results by itself. Including them in the project brief helps identify what the machine trial will demonstrate and which checks will be carried out later with the finished banana package.
Place the forming machine beside the packing operation
The reference machine dimensions are 3650 × 984 × 1870 mm, with a net weight of approximately 1380 kg. A floor plan needs additional space for the blank supply, access to adjustments and the collection of formed boxes. Mark the direction in which cartons should leave the machine and how operators move them to the packing positions. Where an existing conveyor is involved, give its height and the required handover point. The machine footprint is one part of the working layout, rather than the total area required.
The stated supply is 380 V, 50 Hz, three-phase, with 2.5 kW quoted total power. Air consumption is 280 litres per minute at 0.6–0.7 MPa. Share the site’s electrical and compressed-air arrangement before the configuration is finalised. If the banana packing floor has several machines connected to one air system, describe that arrangement too. Installation, collection space and blank storage should be reviewed together so the proposed forming station fits the way the site receives board and uses empty cartons.
Multiple banana sizes and related produce cartons
When a packing programme uses several carton depths or lengths, prepare a separate line in the brief for each box. Include the blank drawing, finished dimensions and required output, even when the supplier describes the boxes as the same family. A change in wall depth may affect folds, glue positions and discharge clearance. The equipment proposal should state which tooling and adjustments are supplied for the agreed designs and how the operator checks the first formed cartons after changing from one size to another.
Other deep fruit cartons can be considered alongside banana boxes if their construction matches the proposed process. Apples or pears, for example, may use a similar general carton family, but their crop name does not determine whether the blank will run. Xunding links this application to the existing fruit box and tray forming categories, then selects the configuration from the actual drawing. Send photos of every related design you want to include, particularly any box with a different base, separate lid or multiple cardboard components.
APPLICATION CONFIGURATION
Configuration reference
These figures describe the proposed application configuration. Confirm the complete blank, production cardboard, tooling, working output and site utilities with Xunding for your project.
| Configuration output range | 20–30 boxes/min |
|---|---|
| Cardboard thickness | 1.5–3 mm |
| Finished box length | 200–550 mm |
| Finished box width | 200–400 mm |
| Finished box height | 150–350 mm |
| Electrical supply | 380 V / 50 Hz, three-phase |
| Quoted total power | 2.5 kW |
| Compressed air consumption | 280 L/min |
| Air pressure | 0.6–0.7 MPa |
| Blank stack height | 500 mm |
| Machine dimensions (L × W × H) | 3650 × 984 × 1870 mm |
| Net weight | Approx. 1380 kg |
Explore the equipment categories
Bring your box drawing and sample to the category that matches its construction.
Fruit tray forming Three-piece fruit boxes Fruit box production linesPLAN YOUR BANANAS PACKING PROJECT
Start with your actual box
Send the flat blank drawing, a finished sample, cardboard thickness, required boxes per minute and your packing-line layout. We will review the forming configuration around your application.
Send your packaging requirementFROM THE FRUIT TO THE BOX
Explore fruit packing applications
See the carton structure, forming process and configuration for each application, with real samples and production footage where available.
Cherry box forming for Chile’s packing season
Explore cherry carton forming for Chile: ventilated box samples, automatic feeding, gluing and stacking, configuration ranges and related fruit box designs.
Read the application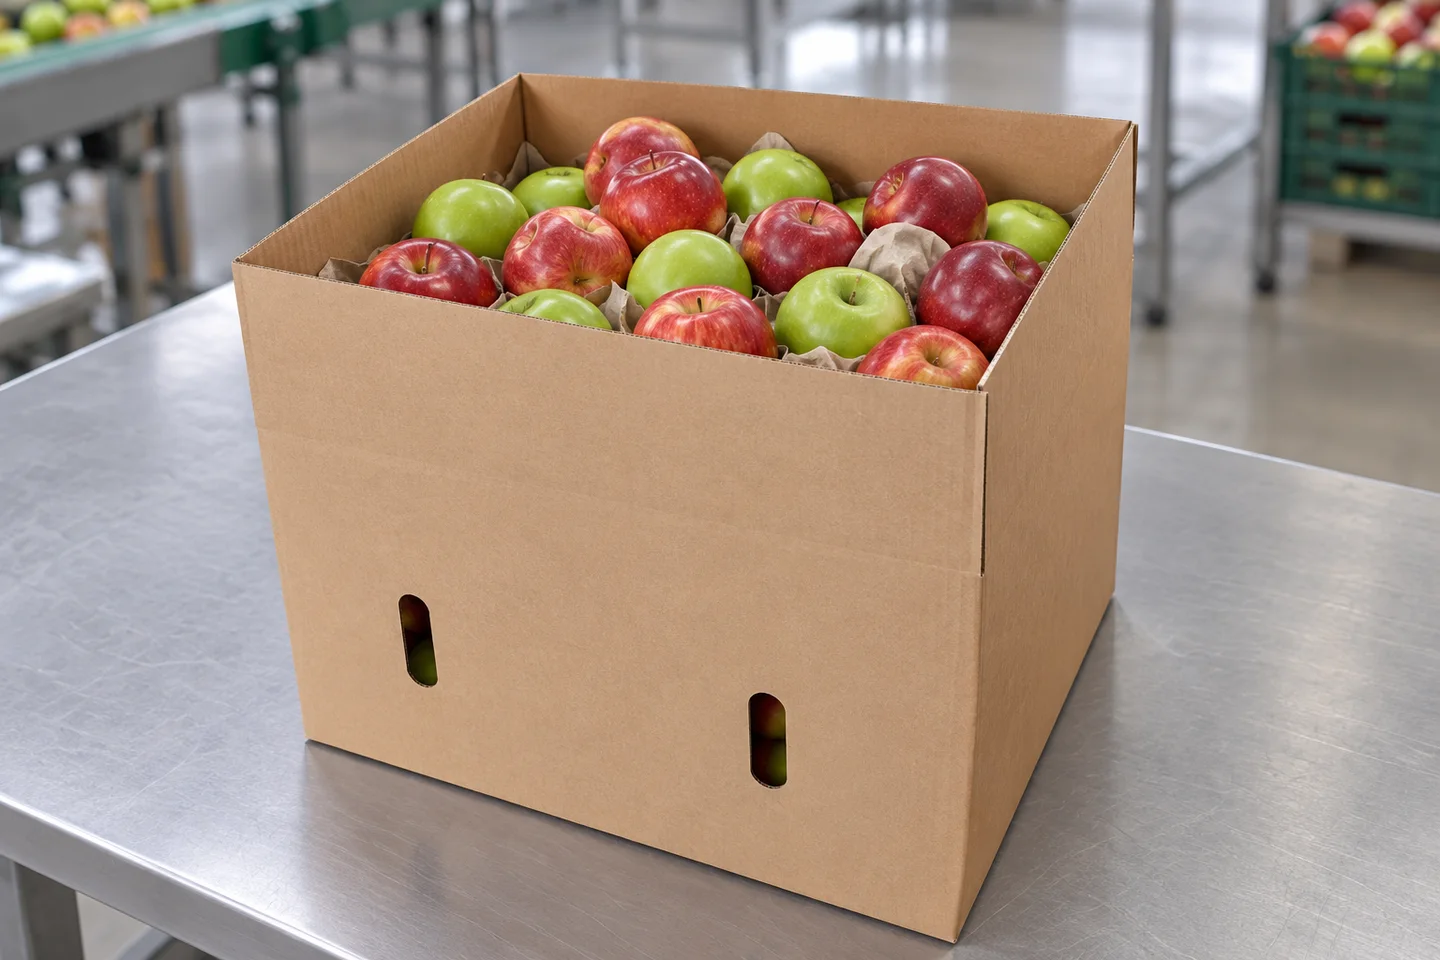
Apple carton forming around the real box design
Explore deep apple carton forming with real box photos and workshop video: elongated ventilation slots, automatic feeding, glue joining and configuration ranges.
Read the application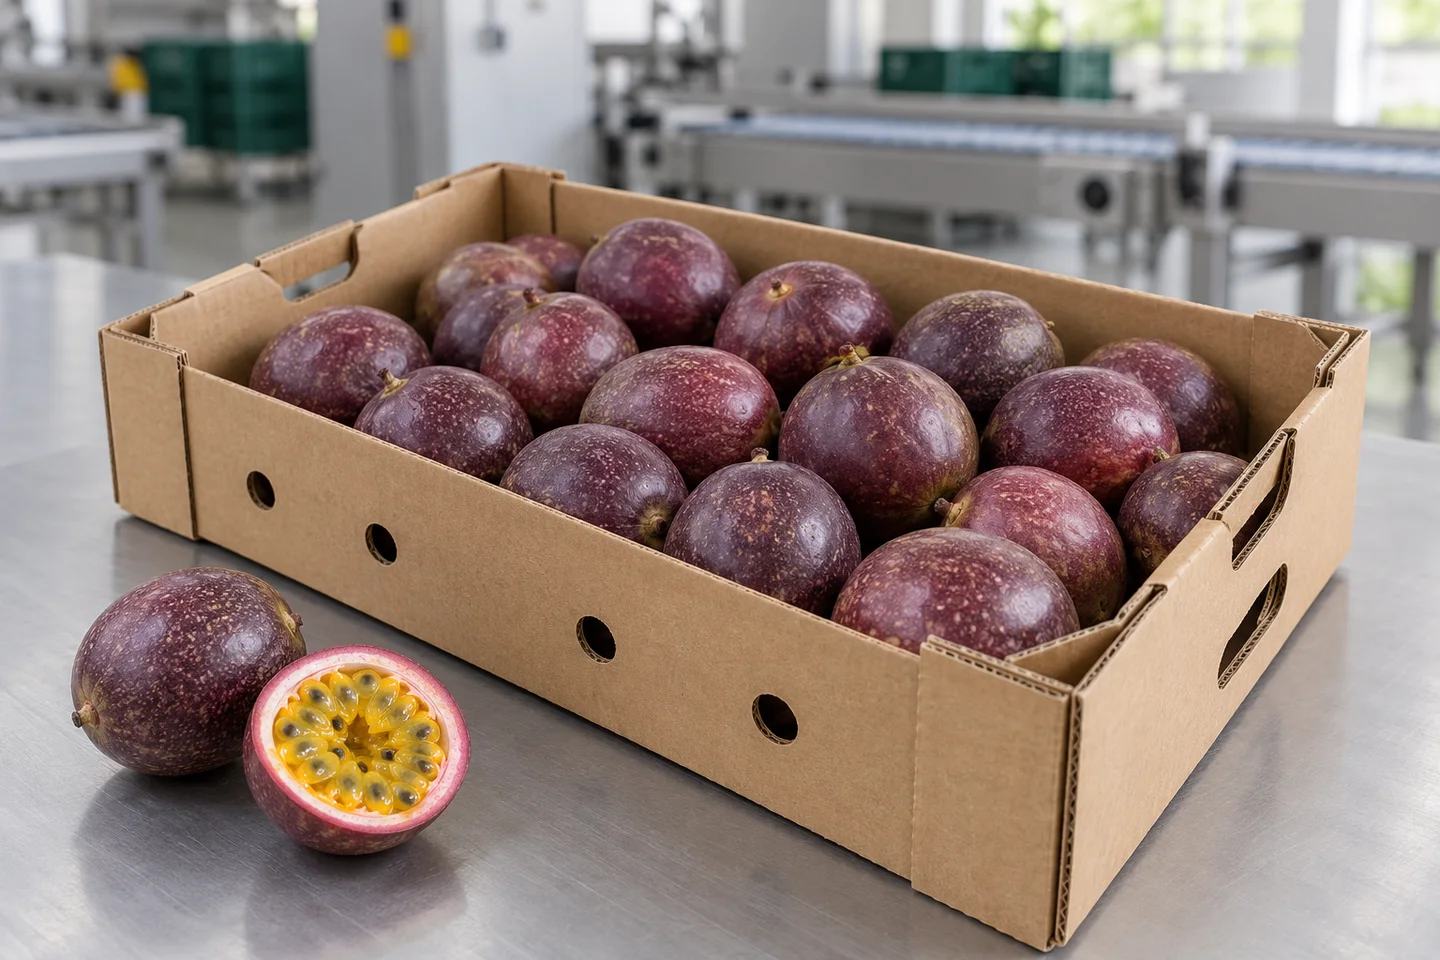
Passion fruit tray forming, from blank to stack
See real passion-fruit carton forming, discharge and stacking footage, with a Siemens-based configuration, board and box ranges, and related produce tray styles.
Read the applicationFruit images are AI illustrations. Real box samples and supplied production videos are labelled within each article.