

You do not need to know a machine model before contacting Xunding. Start with a photograph of the box folded into its finished shape, together with a photograph of the blank opened flat or its die-cut drawing. Include the finished-box length, width and height before we confirm the machine model. Daily output then helps make the configuration recommendation more specific.
First, show the box as it will be used
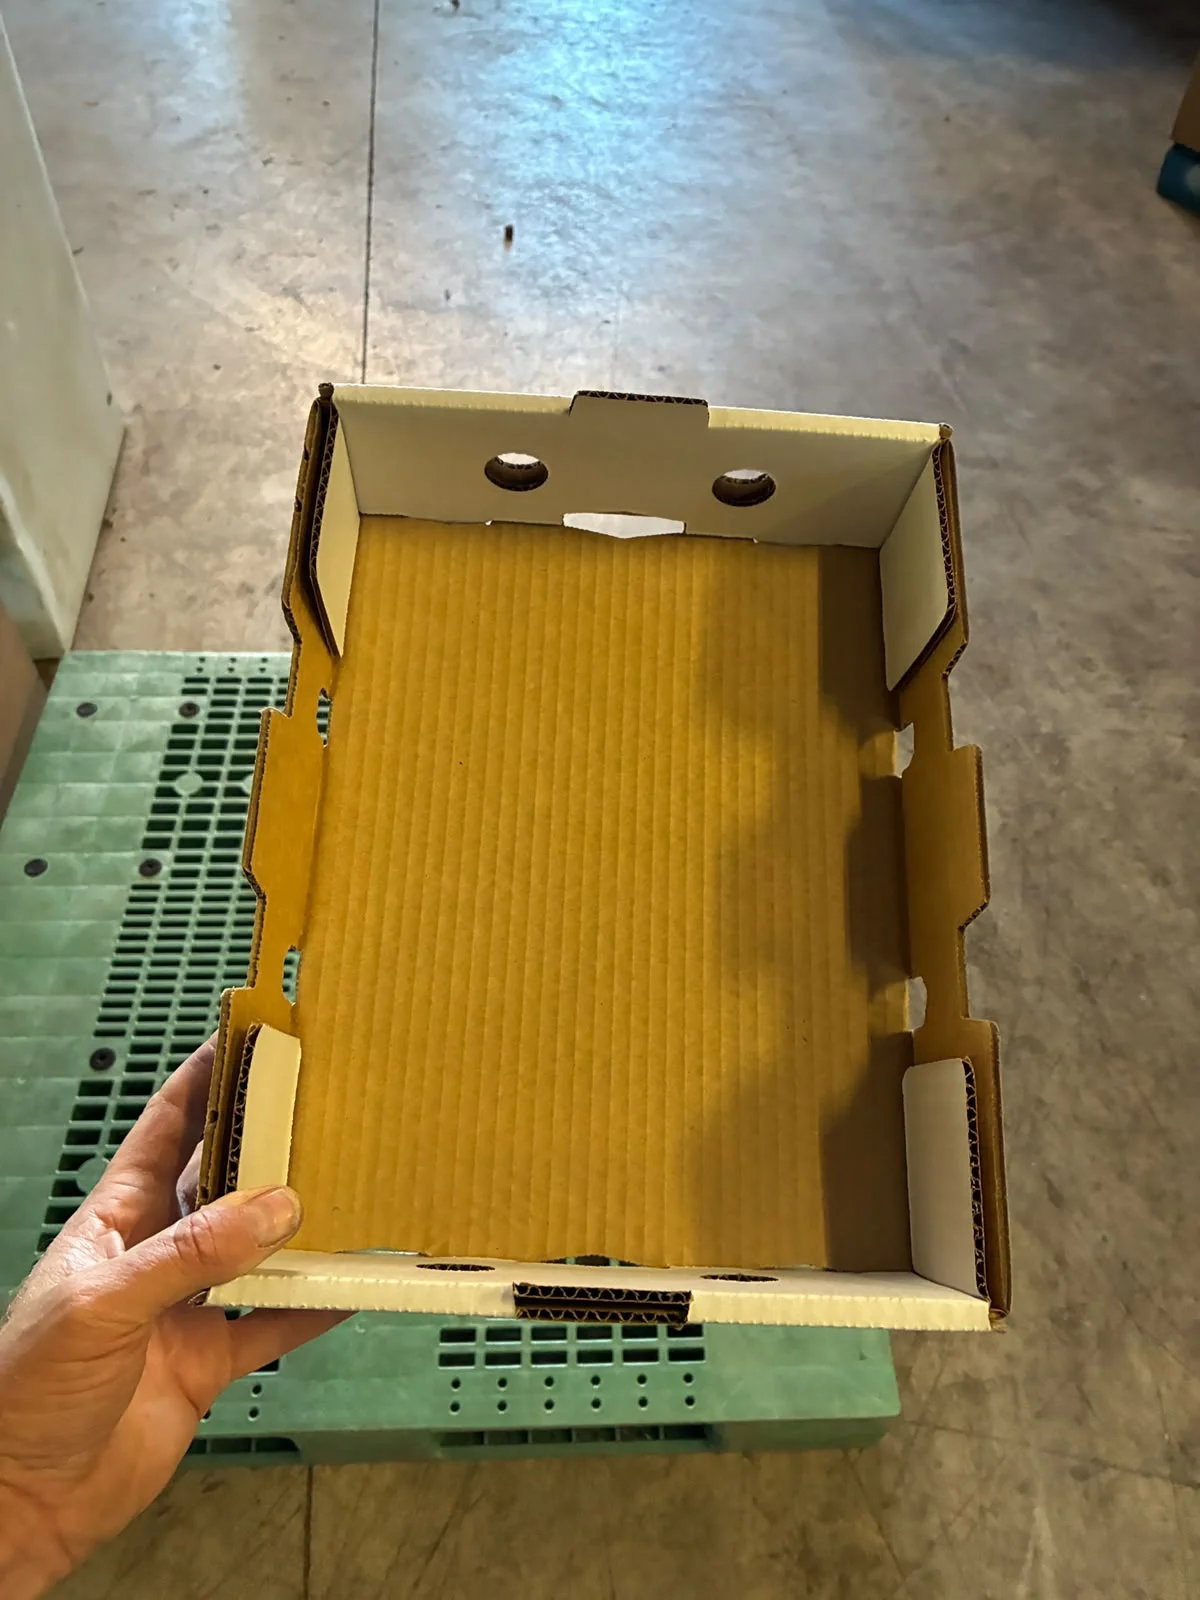
Take a clear photograph of the formed box. Include the corners, walls, lid if present, and the way panels meet. A top view is useful for an open tray; add a side or underside view when a joint, tab or folded panel is hidden.
The formed tray above shows why this view matters. It reveals the upright walls and folded corner panels. A picture of the printing alone would leave those features unclear. Photograph each structure you want to produce, even when several boxes have similar outside dimensions.
Second, show the opened blank or die-cut drawing
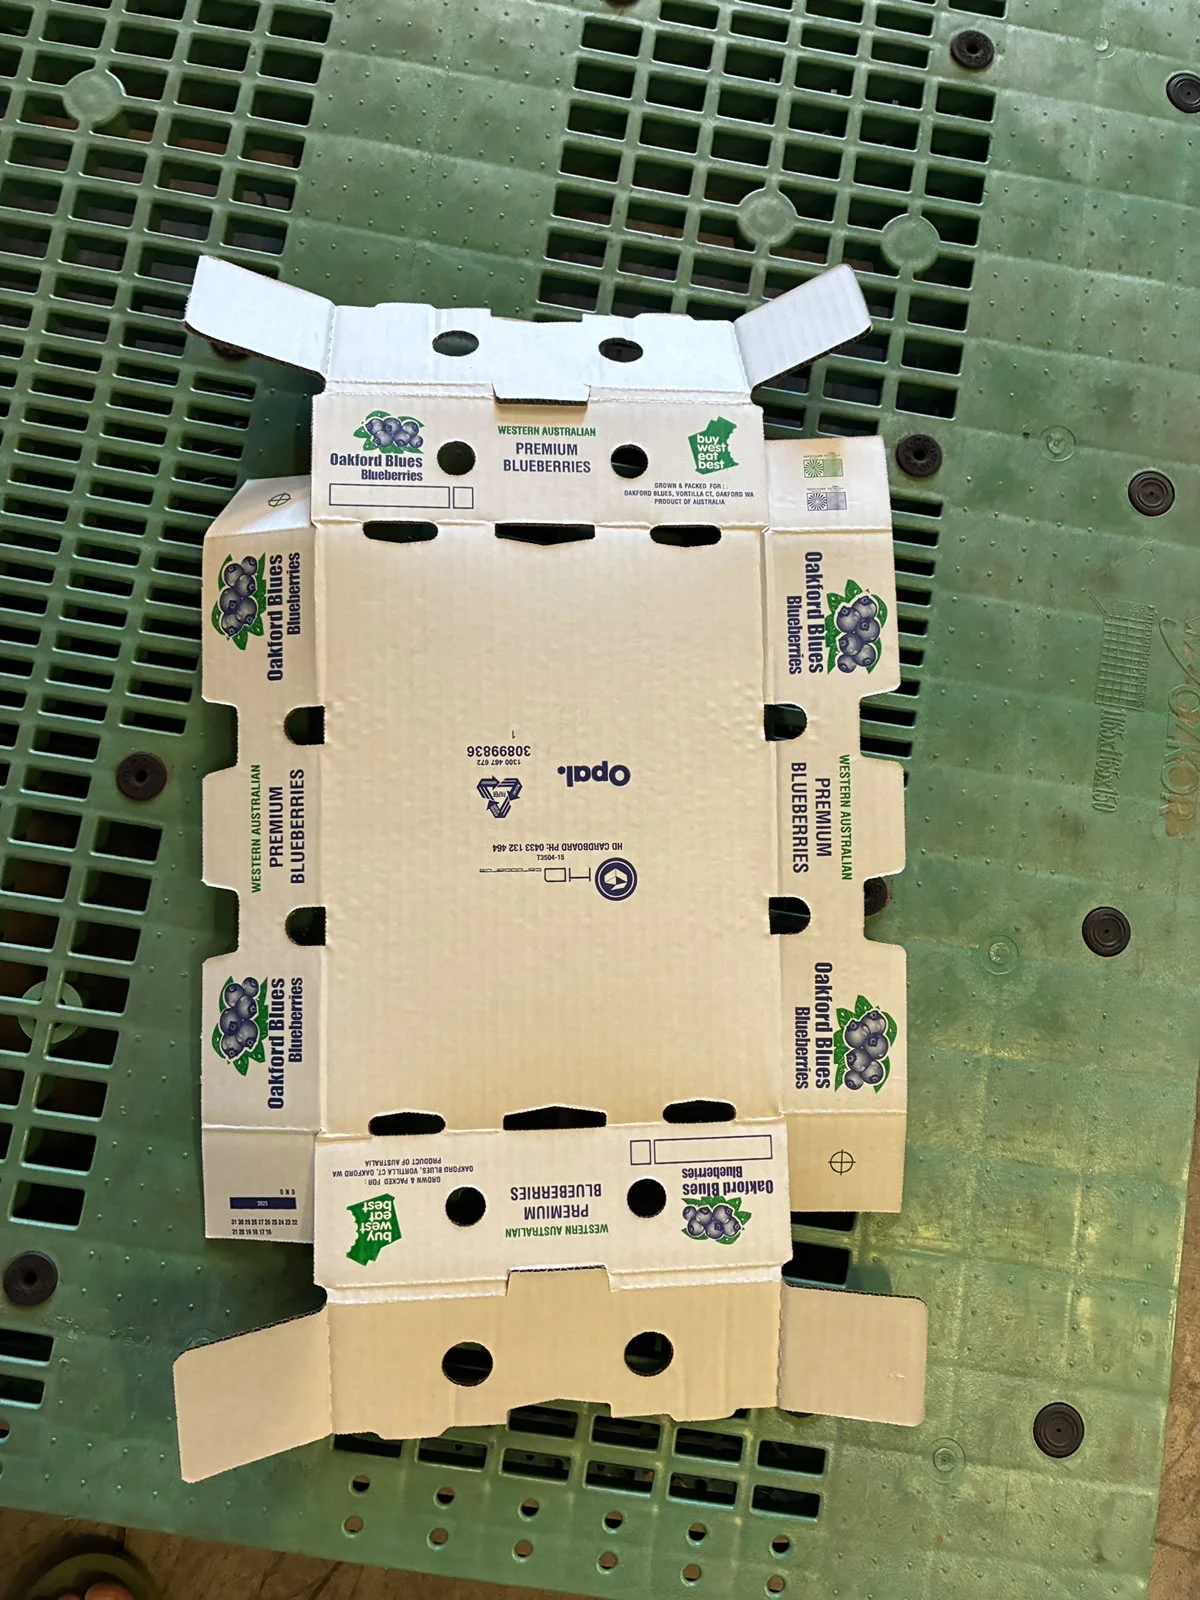
Lay the blank flat and keep its complete outline in the photograph. Show the crease lines, flaps, tabs, openings and panels. If the box uses separate pieces, photograph or draw every piece and show how they join in the finished box.
A die-cut drawing is an alternative to the flat photograph. Send the current drawing with its dimension labels and revision if available. A phone photograph is enough to start a model discussion when a drawing is not ready; a clearer view may be needed where folds or joints are difficult to see.
The opened example below makes the panel layout visible. Compare it with the formed view before sending: both should represent the same box design. Together they give Xunding the structural information needed to identify the machine model.
Compare box structures and catalogue model ranges
Read the orchard enquiry about handling different tray sizes
Then add finished dimensions and the blank size
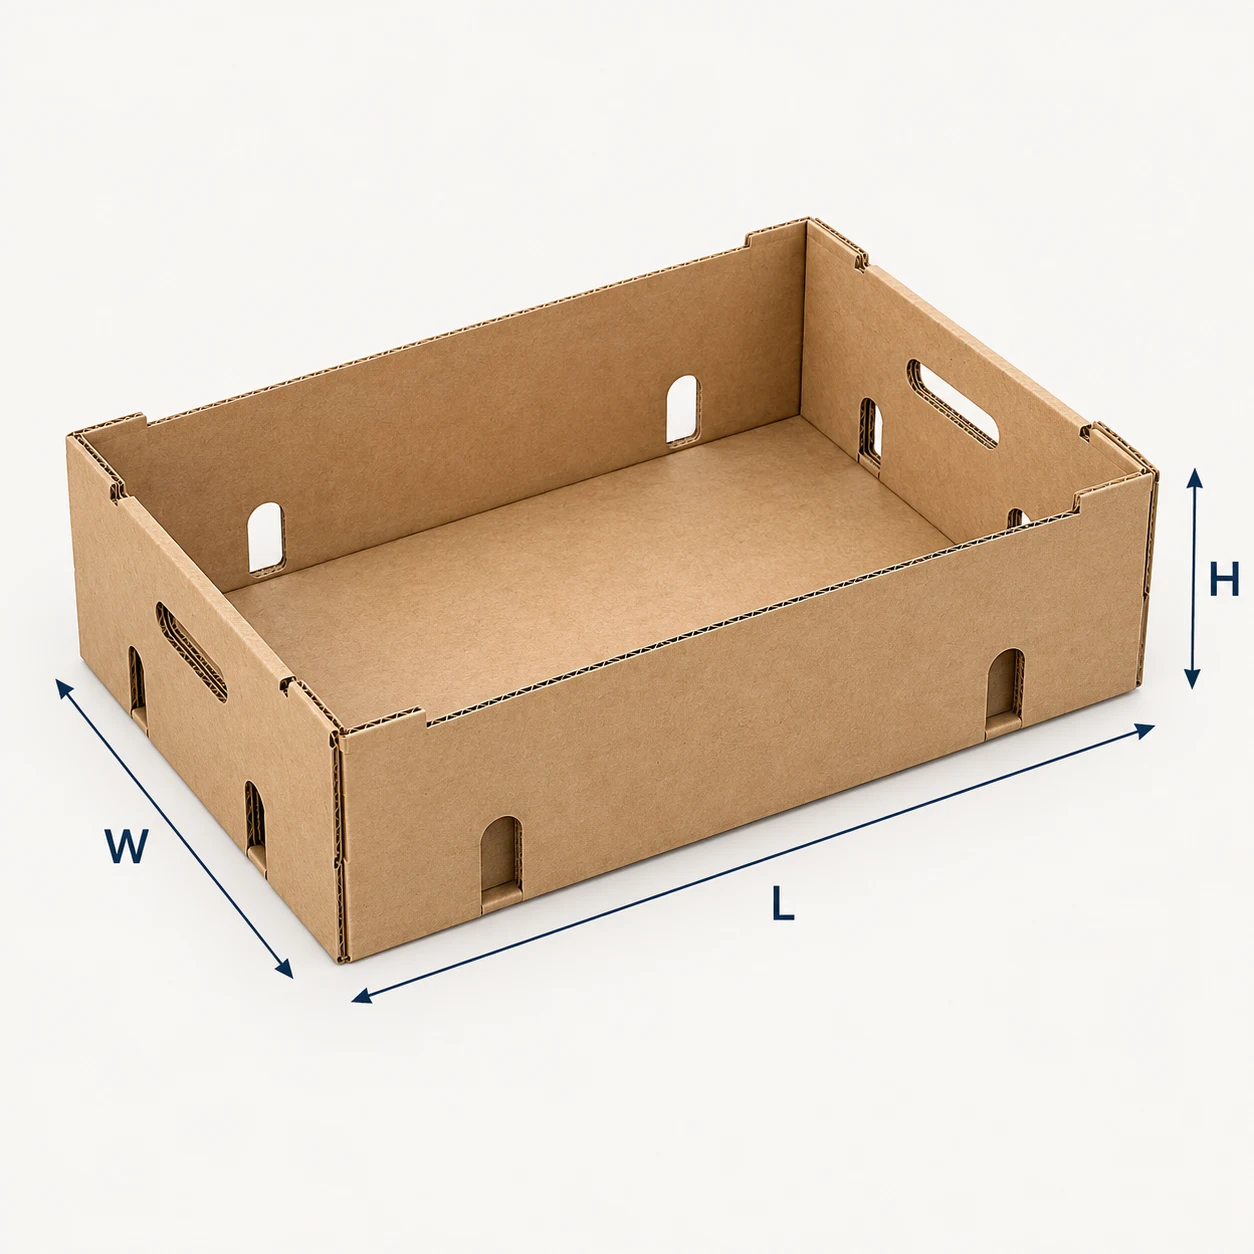
Along with the flat blank or die-cut drawing, provide a formed-box photo and its finished dimensions before confirming the machine model. In the illustration below, L = length, W = width and H = height. Mark the actual measurements for your own box; the illustration shows the measurement directions only.
Give the finished-box length, width and height in millimetres, and mark them on the photograph or drawing. Say whether these are internal or external dimensions. Keep the flat blank dimensions separate: its sheet length and width describe the material entering the machine, rather than the space inside the formed box.
For a lid-and-base design, include both parts. For a three-piece tray, include the base and both end pieces. If several sizes will run on one machine, list each size with its corresponding blank; the largest dimension alone does not describe the complete job.
Xunding model pages separate finished-box L/W/H from flat blank A/B where the catalogue provides both. Use the drawing on that model page to identify the dimensions. A published size range is a starting point for review, not proof that every box structure within it is compatible.
Explain how many boxes you need per day
Tell us the required boxes per day and the available working hours. Include the number of shifts, the mix of box sizes and how often you change designs. If the daily figure changes during a harvest season or a busy order period, give both the usual requirement and the peak requirement.
The same daily total can require different hourly output when working hours differ. Dividing daily required boxes by available production hours gives a planning average. Feeding, replenishment, changeovers and interruptions still need to be considered when confirming the proposed setup.
Ask for an output discussion based on your box and material. Catalogue speeds should not be treated as a guaranteed count of acceptable boxes across an entire shift.
Turn daily demand into accepted trays per hour
Required average accepted trays per hour = required accepted trays per day ÷ available forming hours per day. Keep the units consistent: kilograms of fruit, punnets and filled shipping cartons are not the same count as empty trays. Where packing units differ, give the actual number of packs or products held in each tray before converting the requirement.
Start with the period in which trays must be ready for packing. An eight-hour shift does not necessarily mean eight hours of forming. Record planned breaks, format changes, replenishment and other stops with the person responsible for the production plan. Use known timings or clearly marked planning assumptions; do not apply an invented standard efficiency percentage.
Do not subtract the same interruption twice. If an accepted-output rate was measured over an elapsed trial period that already included replenishment or stops, retain those recorded conditions when comparing it with the daily requirement. State the time basis of each figure so the calculation can be reviewed.
Worked planning examples: the same demand, different windows
The following are arithmetic examples, not measured machine performance. Each uses a hypothetical requirement of 8,000 accepted trays per day. The available hours are stated assumptions; none of the rows is a promise that a Xunding model will achieve that output.
In the first example, 8,000 ÷ 8 = 1,000 accepted trays per hour. With only four available hours, 8,000 ÷ 4 = 2,000. If an eight-hour schedule has one hour allocated to planned stops, the assumed forming window is seven hours: 8,000 ÷ 7 is about 1,143 accepted trays per hour. The third example is a planning adjustment, not a measured changeover or downtime result.
| Illustrative plan | Available forming time | Required average accepted output |
|---|---|---|
| 8-hour window, no time deducted in this example | 8 hours | 1,000 accepted trays/hour |
| Same requirement in a shorter packing window | 4 hours | 2,000 accepted trays/hour |
| 8 scheduled hours less 1 assumed hour of stops | 7 hours | About 1,143 accepted trays/hour |
Plan for the peak packing period and each tray format
Give both the usual daily requirement and the busiest expected packing period. If trays must reach the packing station within a shorter part of the day, state that window separately. Where trays can be formed earlier and stored, explain the collection arrangement and the space available rather than assuming the forming rate must always equal the busiest packing rate.
For several tray formats, list the accepted trays needed for each one and the planned production sequence. Include the changes between them. A total daily count does not show how the machine, tooling and material handling will be organised; one machine changing between formats is different from simultaneous production.
A fruit tray former capacity discussion should connect the forming outlet with the next packing task. Describe how empty trays are collected, stacked or conveyed and when the packing team needs them. The proposed configuration is reviewed against those requirements and the actual blank.
Verify the required output with your actual box
Catalogue speed is not a guaranteed daily output. A calculated requirement helps discuss machine candidates, but compatibility and achievable accepted output depend on the reviewed box, material, configuration and operating conditions. Do not select a model solely because its catalogue rate is above a planning average.
For the sample trial, record the model and configuration, blank revision, board, accepted-box criteria, accepted count and elapsed period. Include the format changes and interruptions that matter to your production. Keep the trial record separate from the planning assumptions, then review whether the proposed setup can support the intended operating window.
Record actual accepted output with the sample-trial checklist
Compare indicative prices and the scope of a project quotation
Add material and site details for the configuration review
After the box structure has identified the model, board thickness, printing or coating, joint requirements and the actual sample help refine the configuration. Include those details if already known. Xunding may request production blanks or a physical sample to check a forming or gluing requirement.
For a connected production line, describe what happens before and after forming. Include the installation country, site power supply, available space and any conveying or stacking needs. These details affect the proposed equipment scope and arrangement.
Browse fruit tray forming models
A short brief you can send with the photographs
Send the two structural views and finished-box L/W/H dimensions before model confirmation. Add the production, material and site details below for the configuration review. If a detail is still being developed, say so and send the information you already have.
| Information | What to send |
|---|---|
| Formed view | Clear photo of the folded box, including corners and any lid |
| Blank view | Complete flat photo or die-cut drawing; every part for a multi-piece box |
| Dimensions | Finished L/W/H in mm; internal or external; separate blank size |
| Production target | Accepted trays per format per day; usual and peak requirements |
| Time basis | Scheduled hours, available forming window and separately identified planned stops |
| Size changes | Each box design and the planned frequency of changeovers |
| Material and site | Known board/coating details, installation country and line requirements |
Send your box photos and production requirement to Xunding
Daily-output FAQ
Can I multiply a catalogue speed by my shift length? Use that only as a theoretical reference. A whole-shift accepted count requires conditions for material, replenishment, changes and interruptions; confirm the proposal using the appropriate trial record.
Should I add a fixed spare-capacity percentage? This guide does not assign one. Provide your demand variation and known operating constraints so the configuration can be reviewed without an arbitrary margin.
What should I send if the harvest forecast is still changing? Send the current usual and peak estimates, label them as estimates, and attach each formed-box view, flat blank and finished dimensions. Update the production brief when the forecast becomes firmer.